A conveyor system is often discussed in terms of belts, chains, speeds and capacities. But these are only part of the engineering equation.
The starting point should be simpler:
What exactly is the conveyor expected to handle?
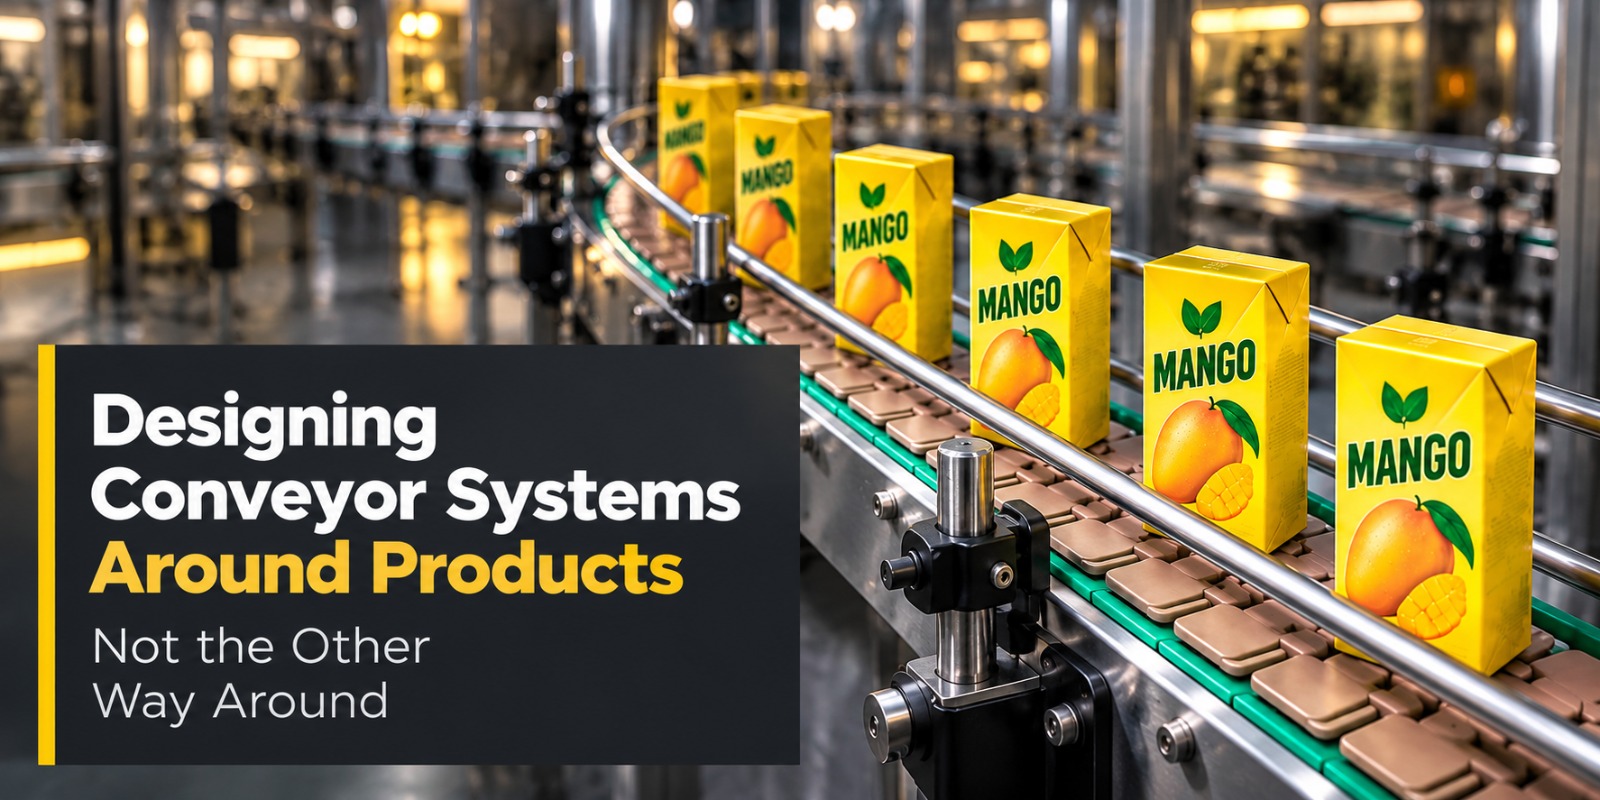
A carton, a food product, a plastic container, a packaged FMCG product and an irregularly shaped component may all need to move from Point A to Point B. Yet the conveyor requirements for each can be very different.
This is why effective conveyor system design should begin with the product and the process—not with a catalogue of available components.
The Product Should Define the Conveyor
Every product interacts differently with a conveyor.
Its size, weight, shape, surface, rigidity, stability and packaging format can influence how it should be conveyed. Even two products of similar weight may require different solutions if one is stable and rigid while the other is flexible or easily tipped.
Before selecting a belt, chain or conveyor configuration, it is important to understand:
- What is being conveyed?
- What are its dimensions and weight?
- How is the product loaded onto the conveyor?
- How does it need to be positioned?
- Does it require controlled movement or accumulation?
- How frequently does the product format change?
- What happens at transfers, curves and discharge points?
These questions provide the foundation for application-specific conveyor engineering.
Conveyor Speed Is Not Just a Number
Higher speed does not automatically mean better conveyor performance.
The appropriate speed depends on how the product behaves while moving. A lightweight package may shift or become unstable at a speed that works perfectly well for a heavier, more stable product.
Similarly, increasing conveyor speed without considering transfers, guide rails, accumulation and downstream processes can create new handling issues.
The objective should therefore be to determine the right operating speed for the application, rather than simply designing for the highest possible speed.
Belt or Chain Selection Should Follow the Application
The choice between different conveyor belts and chains should also be driven by the product and operating environment.
A conveyor handling packaged goods may have different requirements from one handling food products or components in a manufacturing process.
Factors such as:
Product characteristics + load + speed + conveyor layout + operating environment
should collectively guide belt or chain selection.
For modular conveyor systems, this also means considering the interaction between the belt or chain and supporting components such as sprockets, wearstrips and guide profiles.
A component may be technically suitable in isolation but still be inappropriate for the complete application.
Transfers Deserve More Engineering Attention
Many conveyor applications perform well on straight runs but encounter difficulties at transfer points.
Products can rotate, tip, shift or become trapped when moving from one conveyor to another. The issue may not necessarily be with the conveyor belt itself. It can be influenced by the transfer arrangement, product dimensions, conveyor height, speed difference or guide configuration.
This is where application engineering becomes particularly important.
A transfer should be designed around how the product actually moves, not simply around the dimensions of the conveyor.
Guide Rails Should Follow Product Behavior
Guide rails are another example of a component that should be selected according to the application.
Their purpose is not simply to keep a product within the conveyor width. They need to provide appropriate product control without creating unnecessary friction or restricting movement.
When product sizes vary frequently—as they often do in packaging, FMCG and e-commerce operations—the ability to adjust guide rails can become an important consideration in the conveyor design.
The question is not only “Which guide rail should we use?”
It is:
“How does this product need to be guided through this section of the line?”
Supporting Components Are Part of the Engineering
A conveyor system is more than its primary belt or chain.
Sprockets, wearstrips, guide profiles, rollers, shafts and other supporting components all influence how the system performs.
For example, the selection of an appropriate UHMWPE wearstrip can influence the contact between a moving belt or chain and its supporting surface. Similarly, sprocket compatibility and positioning can affect the engagement and movement of a modular belt or chain.
This is why component selection should happen as part of the overall system design—not as a series of independent purchasing decisions.
Designing for the Actual Operating Environment
The physical environment in which the conveyor operates also matters.
Temperature, moisture, cleaning practices, dust, chemicals, operating hours and production conditions can influence the suitability of different materials and components.
A conveyor operating for a few hours a day in a controlled environment may have very different requirements from one operating continuously in a demanding production or fulfilment environment.
Application engineering therefore looks beyond the product itself to understand where, how and for how long the conveyor will operate.
When Product Variety Changes, Conveyor Design Must Adapt
Modern manufacturing and fulfilment operations increasingly handle multiple product formats on the same line.
This introduces another design consideration: flexibility.
If product dimensions, packaging formats or production requirements are likely to change, the conveyor may need adjustable guides, suitable belt configurations, flexible transfer arrangements or other provisions that allow the system to accommodate future requirements.
Designing only for today’s product can create limitations tomorrow.
A well-engineered conveyor considers not just the current application, but the foreseeable operating range.
From Component Selection to Application Engineering
There is an important difference between selling a conveyor component and engineering a conveyor application.
A catalogue can tell you what components are available.
Application engineering asks:
- Where will the component operate?
- What will it interact with?
- What load will it experience?
- What product will it handle?
- What operating conditions will it face?
- How will it affect the rest of the conveyor system?
That shift in approach can make component selection more meaningful and help avoid situations where an individual part appears suitable but does not perform as expected within the complete system.
A Better Starting Point for Conveyor Design
Before finalising a conveyor system, it is worth looking at the application through a sequence of questions:
Product → Process → Environment → Conveyor Configuration → Components
The product determines how it needs to move.
The process determines where and how that movement needs to happen.
The environment determines the operating conditions.
The conveyor configuration brings these requirements together.
And only then should the individual components be selected.
Conclusion
Good conveyor system design is not about fitting a standard conveyor to every application.
It is about understanding what needs to be moved, how it needs to move and what conditions the system will operate under—and then engineering the conveyor around those requirements.
For manufacturers, warehouses, FMCG operations, packaging lines and e-commerce facilities, this approach can make the difference between simply having a conveyor and having a conveyor system that is properly suited to the application.
The right conveyor does not begin with a component catalogue. It begins with the product.
At Ultraplast Chainbelts Pvt. Ltd., conveyor belts, chains and supporting components can be considered as part of the application requirements, helping customers evaluate the appropriate solution based on product handling, operating conditions and conveyor configuration.